Design for Manufacture: Five Drawing Choices That Decide Whether Your Part Machines Cleanly
A manufacturing engineer's DFM checklist: internal corner radii, thin walls, deep holes, standard threads, and tolerance stacking — and how each
Milling, turning, 5-axis, Swiss, materials, finishing and inspection — all under one roof in Chang'an Town, Dongguan.
Nothing here is brokered out to a shop we cannot audit. If your part needs milling, turning, EDM, finishing and inspection, it stays on our floor from raw stock to packed carton.

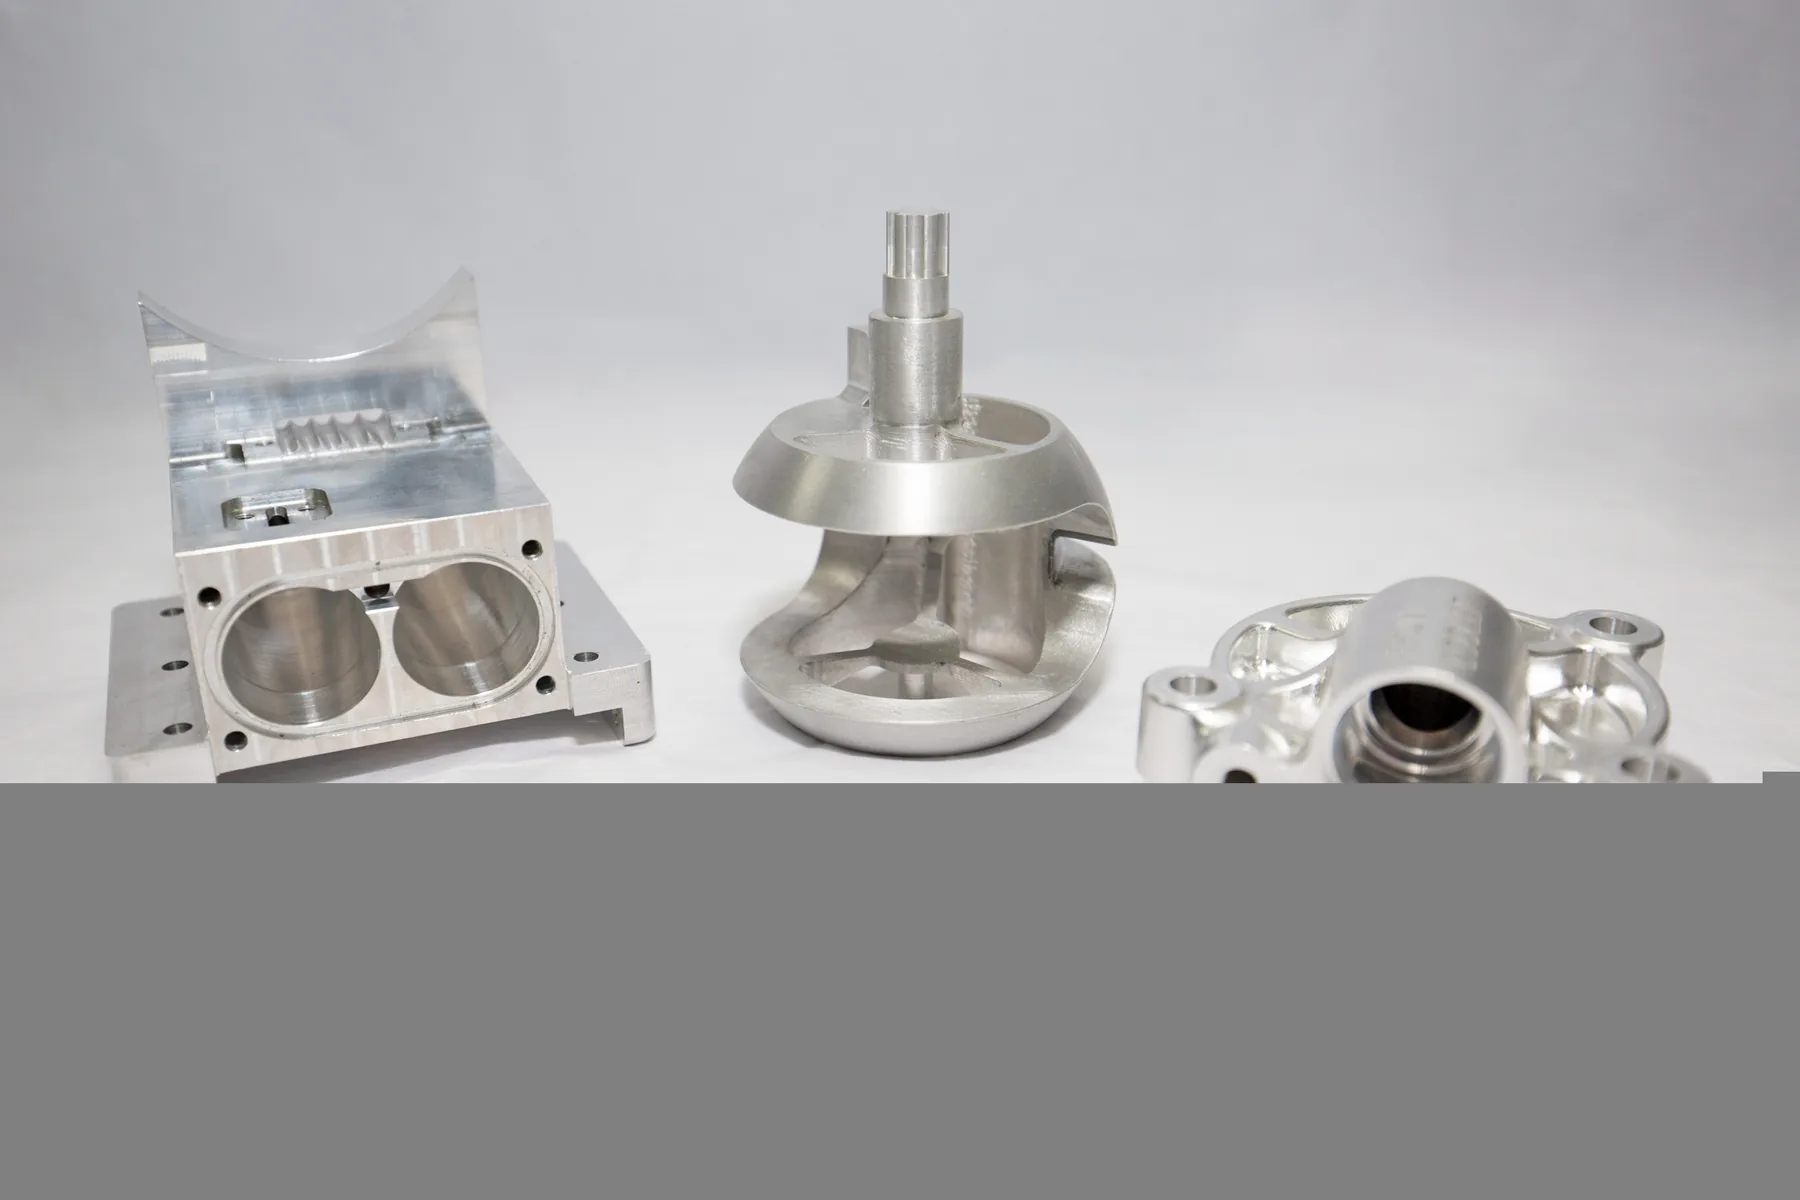
3-axis and 4-axis vertical machining centres for brackets, housings, plates and enclosures, from one-off prototypes to repeat batches.
Learn more
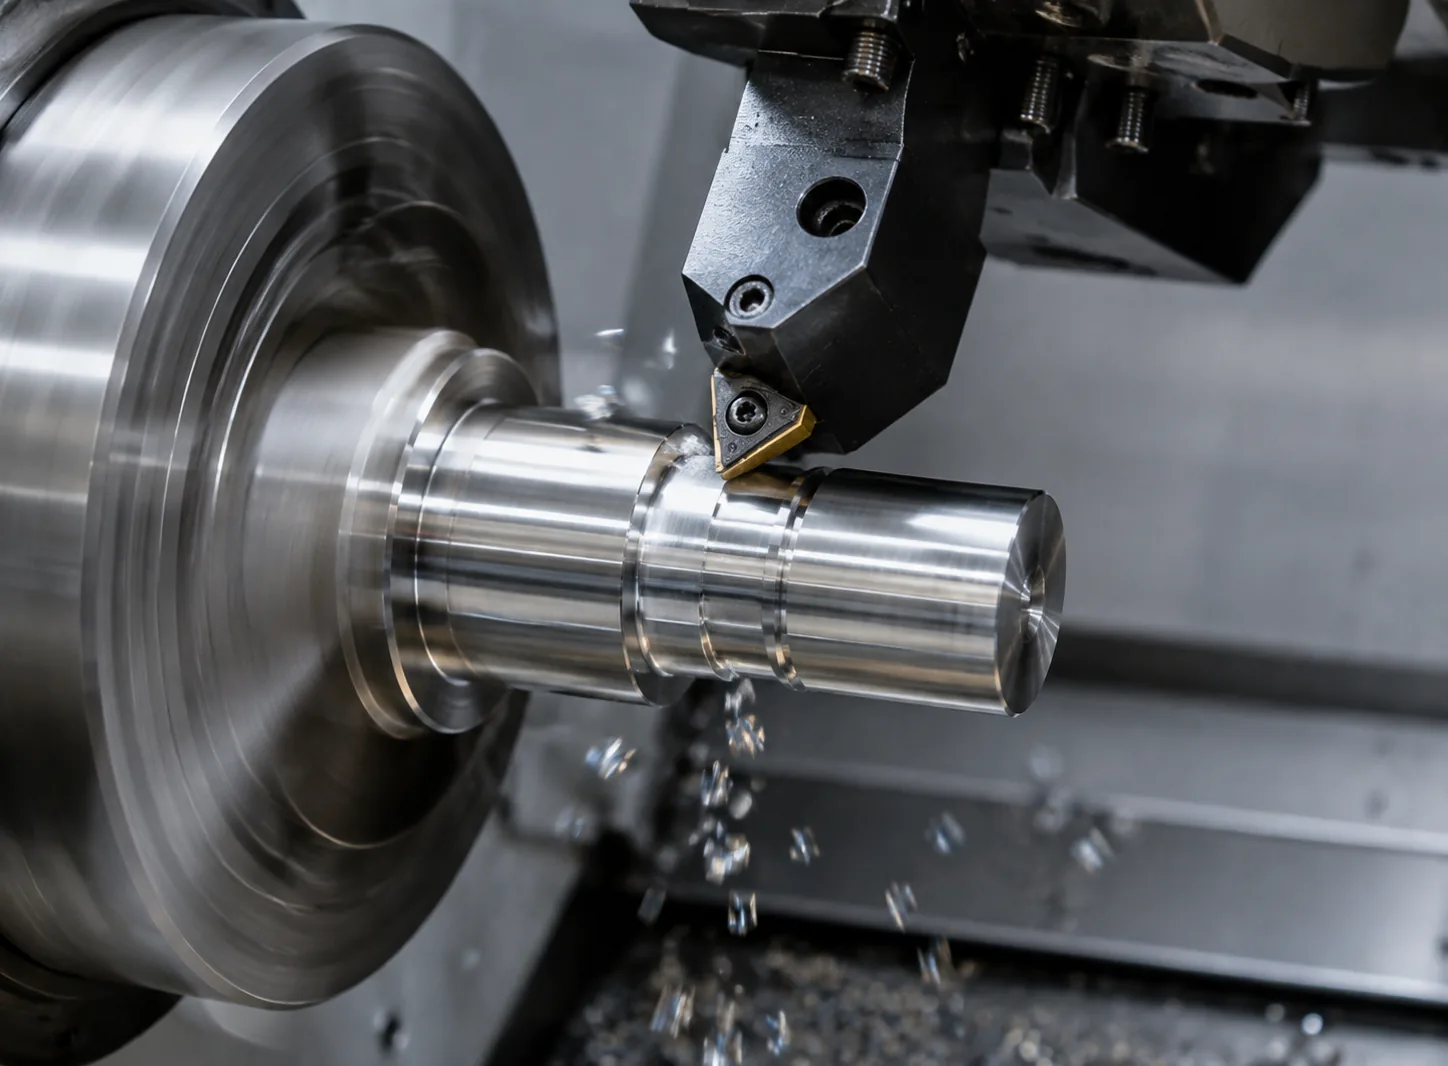
Standard CNC lathes and live-tool turning centres up to Ø380 mm swing. Shafts, bushings, fittings, connectors and threaded components turned complete in one setup.
Learn more
5-axis machining centre (U400A) for complex, multi-face geometry in one setup. Angled features and compound surfaces finished in a single clamping.
Learn more
Swiss-type and sliding-head turning for long slender shafts, micro parts and high-volume turned components with sub-spindle and Y-axis work.
Learn more
Aluminium 6061-T6 is our core material. Stainless steel, brass and engineering plastics are available on request.
Learn more
Anodizing, bead blasting, black oxide, zinc plating and laser engraving, then checked with in-house dimensional inspection.
Learn more| Process | Machines | Typical Tolerance | Volume Sweet Spot |
|---|---|---|---|
| CNC Milling | 3 & 4-axis VMCs | ±0.05 mm typical | No MOQ — prototype to batch |
| CNC Turning | CNC lathes & live-tool centres | ±0.05 mm typical | No MOQ — prototype to batch |
| 5-Axis Machining | 5-axis centre (U400A) | ±0.05 mm typical | No MOQ — prototype to batch |
| Swiss / Sliding-head | Swiss-type turning | ±0.05 mm typical | No MOQ — prototype to batch |
| Turn-Mill | Turn-mill / multi-tasking | ±0.05 mm typical | No MOQ — prototype to batch |

A manufacturing engineer's DFM checklist: internal corner radii, thin walls, deep holes, standard threads, and tolerance stacking — and how each

When does a 5-axis machine lower cost per part instead of raising it? Setup math, fixture count, and a worked 6061 aluminum bracket, fully broken down.

Why Ra alone does not describe a surface, how cutter path, stepover, and nose radius drive finish, and where a surface grinder is the only right tool.
Send your drawings and requirements. Quote, lead time and DFM feedback by email.